In the article High Speed Water Sterilization Using One-Dimensional Nanostructures, silver nanoparticles and carbon nanotubes were used to make a cotton fabric which kills bacteria by applying a low voltage across this conductive material.
The research was completed at Stanford University.
The electrical current that helps do the killing is only a few milliamps at 20volts. The power can be supplied by a small solar panel or a couple 12-volt car batteries. The electrical current can also be generated from a stationary bicycle or by a hand-cranked device.
The full paper can be purchased from the American Chemical Society

Tuesday, August 31, 2010
Friday, August 27, 2010
Presentation on Condensate Polisher ROI
As I alerted in a previous post, Kevin Preising of Res-Kem gave a webcast entitled "Reuse It or Lose It - The Economics of Condensate Polishing". This excellent webcast was given at the GlobalSpec Industrial Processing virtual trade show on August 25 showing how a condensate polisher can pay for itself in 9.6 months! You sve energy and water treatment chemicals.
You can see this presentation any time, day or night through GlobalSpec.
If you are not currently a GlobalSpec subscriber, you will need to register. It is painless and IT'S FREE.
You can see this presentation any time, day or night through GlobalSpec.
If you are not currently a GlobalSpec subscriber, you will need to register. It is painless and IT'S FREE.
Tuesday, August 24, 2010
Fleck and Aquamatic Valve Service Training
On July 27-28, fifteen of Res-Kem's service supervisors and technicians attended a training program on servicing Fleck valves and Aquamatic valves. These people represented the Eastern Service Region and cover areas from Maine to Florida as far west as Pittsburgh.
From this training program, Res-Kem now has additional coverage for softener and filter install, start-up and repair throughout the Eastern Region.
We were fortunate to again have Dave Smith from Pentair to lead the education on the features, maintenance, and repair of Pentair Fleck light industrial and commercial valves. Dave gave a hands-on trouble-shooting and repair training program on Fleck valves. He had the Pentair Fleck 2850 and Fleck 9100 valves on hand so each person could tear down and rebuild each of the valves.

Bob Hader, Service Manager of Res-Kem, led the program to identify, disassemble, and repair common cast iron Aquamatic V42 series, plastic Aquamatic K530 series & plastic K520 series Aquamatic valves. These valves are the most frequently found valves on water
You are welcome to view our YouTube videos on identifying which valve you have, how to use the ordering guides, selecting the correct valve/parts, and how to repair/replace these valves. You can also access the videos through our website.
Michael Urbans gave a demonstration of a dual tank softener in Res-Kem's wet test area. Our service technicians were able to diagnose a 10 year old problem sofetner valve returned from a customer.
If you ever have questions about Fleck or Aquamatic valves, please feel free to contact our expert Mike Polito at 610-358-0717. If you have an Aquamatic. Fleck or Autotrol valve at your plant and need a replacement or replacement parts, please take photos and send them to mpolito@reskem.com.
From this training program, Res-Kem now has additional coverage for softener and filter install, start-up and repair throughout the Eastern Region.
We were fortunate to again have Dave Smith from Pentair to lead the education on the features, maintenance, and repair of Pentair Fleck light industrial and commercial valves. Dave gave a hands-on trouble-shooting and repair training program on Fleck valves. He had the Pentair Fleck 2850 and Fleck 9100 valves on hand so each person could tear down and rebuild each of the valves.

Bob Hader, Service Manager of Res-Kem, led the program to identify, disassemble, and repair common cast iron Aquamatic V42 series, plastic Aquamatic K530 series & plastic K520 series Aquamatic valves. These valves are the most frequently found valves on water

You are welcome to view our YouTube videos on identifying which valve you have, how to use the ordering guides, selecting the correct valve/parts, and how to repair/replace these valves. You can also access the videos through our website.
Michael Urbans gave a demonstration of a dual tank softener in Res-Kem's wet test area. Our service technicians were able to diagnose a 10 year old problem sofetner valve returned from a customer.
If you ever have questions about Fleck or Aquamatic valves, please feel free to contact our expert Mike Polito at 610-358-0717. If you have an Aquamatic. Fleck or Autotrol valve at your plant and need a replacement or replacement parts, please take photos and send them to mpolito@reskem.com.
Friday, July 23, 2010
Economics of Condensate Polishing
On August 25, 2010, Res-Kem's Kevin Preising will make a presentation entitled "Reuse It – Don’t Lose It! The Economics of Condensate Polishing" as part of the Industrial Processing on line tradeshow presented by GlobalSpec.
Abstract of Presentation:
In today's environment of economic pressure and high energy costs, engineers are constantly asked to do more with less. A condensate polisher helps meet this challenge.
Condensate Polishers:
Abstract of Presentation:
In today's environment of economic pressure and high energy costs, engineers are constantly asked to do more with less. A condensate polisher helps meet this challenge.
Condensate Polishers:
- Save energy by reclaiming heat normally sent to drain
- Save water by reducing boiler blow down
- Reduce water treatment chemical usage.
This presentation will use real world examples to show how condensate polishing reduces fuel consumption and minimizes water side fouling in medium- and low-pressure steam plants typical of the food, beverage, and chemical process industries. A follow-up Q&A will address technical aspects of condensate polishing set-up, operation, and maintenance.
Key Take-Aways: - Understand how a condensate polisher and water softener compare
- Learn how to justify the expenditure of a condensate polisher to save energy, water, and chemicals
- Know where to add a condensate polisher to treat your steam condensate
- The ROI of a condensate polisher is less than 10 months!
Kevin's presentation will take place from 3:30 PM - 4:30 PM EDT (12:30 PM - 1:30 PM PDT)
Click here to register for the event.
Wednesday, June 30, 2010
Res-Kem Loses $70,000 Water System Equipment Job
Our service group so successfully helped a food manufacturing company they no longer needed the new system we had quoted for about $70,000!
The System:
Customer has an older dual, 40 cubic foot parallel operating nitrate system required for manufacturing their food products. The normal flow rate is 80 to 85 gpm. The estimated age of the system 15 to 20 years, resin was in service for 10 years but was recently tested and found to be in shape to run another 6 to 12 months. They were in the process of gathering quotes for replacement equipment because they were experiencing low flow, 20 to 30 gpm, reason unknown, from unit #1.
The Problem:
On Tuesday, June 1, the #1 unit failed reducing the product flow to 5 to 10 gpm. As stated above, the normal flow rate is 80 to 85 gpm in a properly operating unit. We were contacted to see if we could service the unit but they could not be down longer than 12 hours due to production demand. They had no information on the system so we didn’t know what type of internals were in the vessel, but believed they were manufactured of black iron.
The Solution:
Res-Kem came on Wednesday, June 2 with two of our installation technicians to service the nitrate removal system. They vacuumed all the resin, gravel support bed but also encountered either anthracite or activated carbon. The internals were found to be manufactured of Schedule 80 PVC and in good condition. One of the technicians backwashed the system prior to refilling the tank and found no blockage within the distributors.
The new resin, Purolite A-520E, was picked up at Purolite by our Res-Kem truck and delivered to the customer the same day of the service. The customer and Res-Kem technicians decided to refill the tank and place it back into service. This was done and the system was operating at 85 gpm.
Start time 8:30AM – Completion 2:00PM
Would have been sooner but they had to bucket the resin into the tank because we could only get a super sack of resin from the manufacturer, due to the urgency, and they had no water pressure to educt the resin into the vessel.
The Bottomline:
They are thrilled with the service and limited downtime and we are now doing the #2 unit, but they are delaying the purchase of the replacement system.
The System:
Customer has an older dual, 40 cubic foot parallel operating nitrate system required for manufacturing their food products. The normal flow rate is 80 to 85 gpm. The estimated age of the system 15 to 20 years, resin was in service for 10 years but was recently tested and found to be in shape to run another 6 to 12 months. They were in the process of gathering quotes for replacement equipment because they were experiencing low flow, 20 to 30 gpm, reason unknown, from unit #1.
The Problem:
On Tuesday, June 1, the #1 unit failed reducing the product flow to 5 to 10 gpm. As stated above, the normal flow rate is 80 to 85 gpm in a properly operating unit. We were contacted to see if we could service the unit but they could not be down longer than 12 hours due to production demand. They had no information on the system so we didn’t know what type of internals were in the vessel, but believed they were manufactured of black iron.
The Solution:
Res-Kem came on Wednesday, June 2 with two of our installation technicians to service the nitrate removal system. They vacuumed all the resin, gravel support bed but also encountered either anthracite or activated carbon. The internals were found to be manufactured of Schedule 80 PVC and in good condition. One of the technicians backwashed the system prior to refilling the tank and found no blockage within the distributors.
The new resin, Purolite A-520E, was picked up at Purolite by our Res-Kem truck and delivered to the customer the same day of the service. The customer and Res-Kem technicians decided to refill the tank and place it back into service. This was done and the system was operating at 85 gpm.
Start time 8:30AM – Completion 2:00PM
Would have been sooner but they had to bucket the resin into the tank because we could only get a super sack of resin from the manufacturer, due to the urgency, and they had no water pressure to educt the resin into the vessel.
The Bottomline:
They are thrilled with the service and limited downtime and we are now doing the #2 unit, but they are delaying the purchase of the replacement system.
Tuesday, June 29, 2010
Industrial UV System Pricing
The Res-Kem web site regularly receives leads for industrial, commercial, residential, and municipal ultraviolet water purifiers. Res-Kem has found that a standalone UV system has become a commodity. With this in mind, Res-Kem will only quote industrial, commercial and municipal UV systems when there is other equipment is being sold.
Examples are a UV system used in combination with rental deionization and filtration systems, or a UV system as part of our modular ultrapure water (UPW) system.
Examples are a UV system used in combination with rental deionization and filtration systems, or a UV system as part of our modular ultrapure water (UPW) system.
Friday, June 11, 2010
RO Systems for Industrial & Commerical Water Treatment
Res-Kem now offers four new Reverse Osmosis (RO) system series with product flow rates of up to 700 gpm.
XL Series RO 12 - 700 GPM
These RO systems can control your entire water treatment system. By simply activating standard features through a Color Panelview Plus touchscreen HMI, the operation of the pretreatment, RO system, RO tank level, recirculation pump, and post-treatment DI is coordinated, controlled and monitored. Virtually seamless operation of any system is realized. Through the X-Web™ service, we can be remotely monitor the entire XL Series RO system and alarms.
Built to last design with stainless steel frame and high pressure piping, high efficiency stainless steel multi-stage Grundfos pump with TEFC motor and Dow Filmtec XLE 440 low energy membranes. XL Series RO has features only available on custom industrial systems.
CL and CLD Series RO 3,200 - 69,000 GPD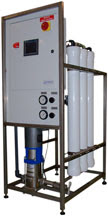
These RO systems can control your entire water treatment system. By simply activating standard features through a Color Panelview Plus touchscreen HMI, the operation of the pretreatment, RO system, RO tank level, recirculation pump, and post-treatment DI is coordinated, controlled and monitored. Virtually seamless operation of any system is realized. Through the X-Web™ service, we can be remotely monitor the entire system and alarms .
These system have a rugged design with stainless steel frame and high pressure piping, high efficiency stainless steel multi-stage pump with TEFC motor and Dow Filmtec XLE 4040 low energy membranes. These systems have features only available on custom industrial systems.
CLT Series RO 3,200 - 34,500 GPD
The CLT Series RO has a rugged design with stainless steel frame and high pressure piping, high efficiency stainless steel multi-stage pump with TEFC motor and Dow Filmtec XLE 4040 low energy membranes. Has features only available on custom industrial systems.
ML Series RO 1,500 - 8,900 GPD
The ML Series RO has a rugged design with stainless steel frame and high pressure piping, high efficiency positive displacement pump and Dow Filmtec XLE 4040 low energy membranes. These systems have features only available on custom industrial systems
XL Series RO 12 - 700 GPM

These RO systems can control your entire water treatment system. By simply activating standard features through a Color Panelview Plus touchscreen HMI, the operation of the pretreatment, RO system, RO tank level, recirculation pump, and post-treatment DI is coordinated, controlled and monitored. Virtually seamless operation of any system is realized. Through the X-Web™ service, we can be remotely monitor the entire XL Series RO system and alarms.
Built to last design with stainless steel frame and high pressure piping, high efficiency stainless steel multi-stage Grundfos pump with TEFC motor and Dow Filmtec XLE 440 low energy membranes. XL Series RO has features only available on custom industrial systems.
CL and CLD Series RO 3,200 - 69,000 GPD

These RO systems can control your entire water treatment system. By simply activating standard features through a Color Panelview Plus touchscreen HMI, the operation of the pretreatment, RO system, RO tank level, recirculation pump, and post-treatment DI is coordinated, controlled and monitored. Virtually seamless operation of any system is realized. Through the X-Web™ service, we can be remotely monitor the entire system and alarms .
These system have a rugged design with stainless steel frame and high pressure piping, high efficiency stainless steel multi-stage pump with TEFC motor and Dow Filmtec XLE 4040 low energy membranes. These systems have features only available on custom industrial systems.
CLT Series RO 3,200 - 34,500 GPD
The CLT Series RO has a rugged design with stainless steel frame and high pressure piping, high efficiency stainless steel multi-stage pump with TEFC motor and Dow Filmtec XLE 4040 low energy membranes. Has features only available on custom industrial systems.
ML Series RO 1,500 - 8,900 GPD

The ML Series RO has a rugged design with stainless steel frame and high pressure piping, high efficiency positive displacement pump and Dow Filmtec XLE 4040 low energy membranes. These systems have features only available on custom industrial systems
Tuesday, May 25, 2010
Softener Service at Power Plant in New Jersey
After reviewing our blog posts over the past 4+ years, I realized we have not talked much about our site service team. Our normal service area is in New Jersey, Eastern Pennsylvania, Delaware, and Maryland. On a case-by-case basis we have gone substantially further.
Situation:
At a power plant in coastal New Jersey, a triple water softener system needed to have a media exchange. Each steel vessel has 20 cuft of softening resin. Res-Kem brought our trailer mounted vacuum.

Services Provided:
Manned by two Res-Kem service people, the entire process of resin removal, underdrain inspection, and refilling took only 5 hours to complete from start to finish. "We could have been done about 1-1.5 hours sooner, but we couldn't shutdown all three units at once" said Joe Urbans III Res-Kem lead rebed technician because we needed to work around the plant's operation.
Testimony:
Our sales representative at the site stated "The Res Kem team was extremely professional! They executed all of the work safely, they worked quickly and efficiently - regularly checking in with the customer. The station engineer was very pleased with the work".
Situation:
At a power plant in coastal New Jersey, a triple water softener system needed to have a media exchange. Each steel vessel has 20 cuft of softening resin. Res-Kem brought our trailer mounted vacuum.

Services Provided:
Manned by two Res-Kem service people, the entire process of resin removal, underdrain inspection, and refilling took only 5 hours to complete from start to finish. "We could have been done about 1-1.5 hours sooner, but we couldn't shutdown all three units at once" said Joe Urbans III Res-Kem lead rebed technician because we needed to work around the plant's operation.
Testimony:
Our sales representative at the site stated "The Res Kem team was extremely professional! They executed all of the work safely, they worked quickly and efficiently - regularly checking in with the customer. The station engineer was very pleased with the work".
Thursday, April 29, 2010
Nalco Acquires Res-Kem and General Water-Denise’s Story
On April 1st, I was fortunate enough to have sold my company, which I have been building for over 26 years, to Nalco Company. We are a wholly owned subsidiary now and our official name is Res-Kem LLC although we will continue to go by Res-Kem General Water.
As with every privately held business in America it is imperative to have a succession plan in place. As responsible business owners, my business partner and husband Bob Hader and I developed a business and team that would continue to thrive whether or not we are able to work. The team of people who work at our company are the best at what they do and I’ve worked hard to make sure no one was irreplaceable, including me.
I know things don’t always go as planned. I wasn’t looking to sell the business, we had a great 2009 in spite of the recession, but we were at a point where it was time to consider the next steps. These steps always include investing money in the business and it was time to consider all of my options. During the past year I’ve explored all the options and and was lucky enough to have been approached by Nalco during this evaluation.
My goals were to:
1. Continue to grow the business and secure the employment of my co-workers. As a family business, my coworkers include two brothers, a nephew, and many people who are like family. Those of you in small businesses know what I’m talking about.
2. Continue to take care of all of customers in the same fashion. We have a reputation to uphold. We are a business to business company but most importantly we’re a people company. We work hard for and like our customers.
3. Expand the company so rewarding manufacturing jobs will be available for the next generation.
4. Sell the company to people who would like for me to continue operating it. I may be in denial about my age, but I’m still not old enough to retire!
5. Make a deal with people I like – I had to like the people I would sell the company to.
So here’s the bottom line. I have accomplished all my goals and am excited for the future. As I said before the acquisition, we are not a chemical company. We distribute, service, and assemble water treatment equipment including service DI. I want to assure each of our customers using a different chemical company that we will continue to do business as always and not be bringing in the local Nalco rep. We are simply doing for Nalco the same things we’ve been doing for years – supplying equipment, services and SDI.
As with every privately held business in America it is imperative to have a succession plan in place. As responsible business owners, my business partner and husband Bob Hader and I developed a business and team that would continue to thrive whether or not we are able to work. The team of people who work at our company are the best at what they do and I’ve worked hard to make sure no one was irreplaceable, including me.
I know things don’t always go as planned. I wasn’t looking to sell the business, we had a great 2009 in spite of the recession, but we were at a point where it was time to consider the next steps. These steps always include investing money in the business and it was time to consider all of my options. During the past year I’ve explored all the options and and was lucky enough to have been approached by Nalco during this evaluation.
My goals were to:
1. Continue to grow the business and secure the employment of my co-workers. As a family business, my coworkers include two brothers, a nephew, and many people who are like family. Those of you in small businesses know what I’m talking about.
2. Continue to take care of all of customers in the same fashion. We have a reputation to uphold. We are a business to business company but most importantly we’re a people company. We work hard for and like our customers.
3. Expand the company so rewarding manufacturing jobs will be available for the next generation.
4. Sell the company to people who would like for me to continue operating it. I may be in denial about my age, but I’m still not old enough to retire!
5. Make a deal with people I like – I had to like the people I would sell the company to.
So here’s the bottom line. I have accomplished all my goals and am excited for the future. As I said before the acquisition, we are not a chemical company. We distribute, service, and assemble water treatment equipment including service DI. I want to assure each of our customers using a different chemical company that we will continue to do business as always and not be bringing in the local Nalco rep. We are simply doing for Nalco the same things we’ve been doing for years – supplying equipment, services and SDI.
Monday, April 19, 2010
Nalco Acquires Res-Kem and General Water
It has been a very busy day at Res-Kem and General Water. All of us are being contacted by many of our customers after reading the news release about Nalco's acquisition of the Res-Kem and General Water businesses. All of us in Res-Kem and General Water are excited to be part of this organization. Also, as stated in the news release, "This acquisition improves Nalco's ability to provide customers with the equipment, supplies and accessories for a total industrial water solution in general industry markets throughout the Northeastern United States, specifically in Pennsylvania, New Jersey, Delaware and Maryland."
Subscribe to:
Posts (Atom)